Medicine Packaging Boxes: Essential Considerations for Safe and Informative Pharmaceutical Packaging
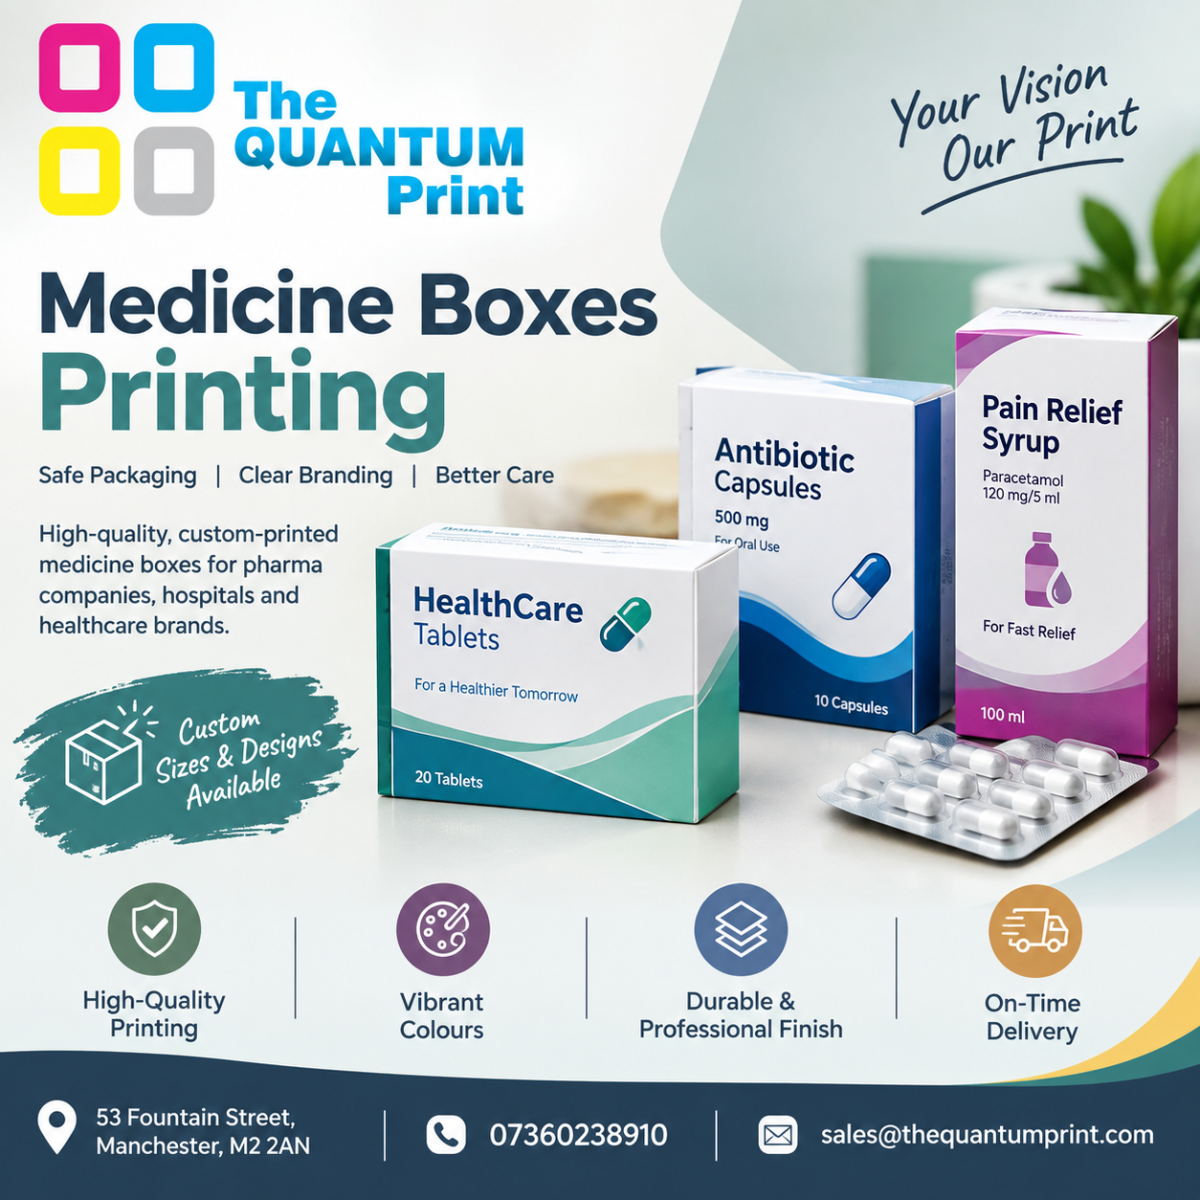
Medicine Boxes Printing is an important part of this process because printed packaging helps manufacturers and distributors present product information consistently while maintaining a professional appearance.
Pharmaceutical packaging plays an important role in protecting medicines, communicating essential information, and supporting safe handling throughout the supply chain. From prescription tablets and capsules to liquid formulations and over-the-counter treatments, packaging must meet practical requirements while remaining clear, durable, and suitable for its intended purpose. As the pharmaceutical industry evolves, businesses are paying greater attention to material selection, product identification, sustainability, and packaging design.
Medicine Boxes Printing is an important part of this process because printed packaging helps manufacturers and distributors present product information consistently while maintaining a professional appearance. Effective packaging combines structural protection with accurate labelling, making it easier for healthcare professionals, pharmacists, and consumers to identify and handle medicinal products appropriately.
1. Why Pharmaceutical Packaging Matters
Medicine packaging serves several purposes beyond containing a product. It helps protect medicines from physical damage, supports identification, and provides space for essential instructions and regulatory information.
Depending on the medicine and its storage requirements, packaging may need to protect against moisture, light, contamination, or accidental opening. The appropriate solution depends on the formulation, shelf-life requirements, distribution conditions, and compatibility of the packaging materials.

Well-designed pharmaceutical packaging can offer several benefits:
- Product protection: Helps protect medicine containers and contents from damage during storage and transportation.
- Clear identification: Makes it easier to distinguish products, strengths, formulations, and pack sizes.
- Information accessibility: Provides space for dosage instructions, warnings, ingredients, batch details, and expiry information where required.
- Supply-chain efficiency: Supports organised storage, stock management, and product identification.
- Patient understanding: Helps present instructions and warnings in a readable, structured format.
Packaging must be designed with the product’s specific requirements in mind. A carton intended for blister-packed tablets, for example, may require different dimensions and structural features from a box designed to hold a medicine bottle.
2. Choosing Suitable Medicine Packaging Boxes
Selecting appropriate Medicine Packaging Boxes involves balancing protection, usability, printing requirements, and applicable regulations. The packaging material should be strong enough for distribution while remaining suitable for the product’s intended storage and handling conditions.
Paperboard cartons are widely used for secondary pharmaceutical packaging because they can accommodate printed information and provide an additional layer of protection around primary containers, such as blister packs and bottles. However, a cardboard carton alone does not necessarily provide a moisture barrier, child resistance, or tamper evidence. These functions may require additional packaging components.
Important considerations include:
- Material strength: Choose a board grade that can withstand expected handling and transport conditions.
- Dimensions and fit: Ensure the carton accommodates the product without excessive movement or unnecessary material.
- Closure design: Select a closure appropriate to the product, packaging process, and applicable safety requirements.
- Storage conditions: Consider humidity, temperature, light exposure, and the medicine’s stability requirements.
- Printing compatibility: Confirm that the selected material supports the required text, graphics, and finishing processes.

Manufacturers should also evaluate packaging performance through suitable testing. Drop tests, compression assessments, and checks of closure integrity can help identify weaknesses before large-scale production.
3. The Role of Design and Printing in Medicine Box Packaging
Effective medicine box packaging combines functional construction with clear visual communication. Pharmaceutical cartons often contain considerable information, so the layout must help readers locate important details without making the design unnecessarily complicated.
A useful design begins with a clear information hierarchy. Product names, strengths, dosage forms, warnings, and other critical details should be presented consistently and legibly. Typography, spacing, contrast, and alignment all influence how easily information can be understood.
Professional medicine packaging box design should also consider the following practical points:
- Readable typography: Use appropriate font sizes and sufficient contrast, particularly for safety-critical information.
- Accurate colour reproduction: Maintain consistent colours where they help distinguish products or strengths.
- Barcode readability: Allow sufficient space for barcodes and ensure they can be scanned reliably.
- Print quality control: Check for missing text, smudging, colour inconsistencies, and alignment errors.
- Proof approval: Review artwork carefully before authorising full production.
The printing process may involve digital or offset printing, depending on order quantities, artwork complexity, turnaround requirements, and budget. Digital printing can be useful for shorter runs or product variations, while offset printing may suit larger production volumes.
The Quantum Print provides an example of a packaging supplier offering pharmaceutical carton options through its medicine packaging range. When evaluating any supplier, businesses should assess print consistency, material specifications, production capabilities, and the accuracy of supplied packaging information rather than relying on appearance alone.
4. Regulatory Information, Quality Control, and Common Challenges
Pharmaceutical packaging in the United Kingdom must be developed with applicable legislation and product-specific requirements in mind. Depending on the medicine, packaging and labelling may need to include information such as the product name, strength, active ingredients, dosage instructions, warnings, batch number, expiry date, and storage conditions.
Requirements can differ according to the medicine category and intended market. Prescription medicines may also be subject to additional requirements concerning patient information leaflets, anti-tampering features, and safety systems. Businesses should verify the relevant requirements with qualified regulatory professionals and current guidance from the Medicines and Healthcare products Regulatory Agency (MHRA).

Several common challenges deserve particular attention:
Printing errors: Incorrect strengths, outdated instructions, or missing warnings can create serious risks. Version-controlled artwork, proof checking, and documented approval procedures help reduce these errors.
Packaging damage: Weak cartons or unsuitable dimensions can result in crushed corners, damaged closures, or movement inside the pack. Material testing and structural design reviews help address these problems.
Barcode problems: Poor contrast, incorrect dimensions, or printing defects can prevent scanning. Barcode verification should form part of quality control.
Changing regulations: Updates to product information or regulatory requirements may make existing packaging artwork unsuitable. A controlled review process helps ensure that revised packaging is approved before production.
Quality assurance should continue beyond the initial design stage. Incoming material checks, production inspections, traceability records, and final packaging assessments contribute to consistent results.
5. Sustainability and Emerging Packaging Trends
Sustainability is becoming an important consideration across the UK packaging industry. Pharmaceutical businesses are exploring recyclable paperboard, reduced material usage, efficient carton designs, and printing processes that minimise avoidable waste.
However, sustainability decisions must not compromise medicine protection or regulatory compliance. Recyclability depends on the complete packaging structure, coatings, adhesives, inks, and local recycling facilities. Any proposed material change should therefore be assessed for performance, product compatibility, and disposal requirements.

Digital production technologies and improved artwork management are also helping businesses handle smaller batches, product variations, and packaging revisions more efficiently. At the same time, automation and inspection systems can support better detection of printing defects and production inconsistencies.
For businesses planning new packaging, the most effective approach is to evaluate environmental objectives alongside product safety, material performance, manufacturing requirements, and total lifecycle impact.
Final Takeaway
Reliable pharmaceutical packaging depends on more than an attractive carton. It requires suitable materials, accurate printed information, thoughtful structural design, consistent quality control, and compliance with relevant regulations. By addressing these factors early, manufacturers and distributors can reduce avoidable errors, improve handling, and support clearer communication throughout the medicine supply chain.
Whether reviewing existing cartons or developing new packaging, businesses should prioritise product protection, readable information, verified artwork, and appropriate testing. These fundamentals help ensure that pharmaceutical packaging remains practical, dependable, and fit for its intended purpose
Contact Us : https://www.thequantumprint.com/contact-us/
About Us : https://www.thequantumprint.com/about-us/
Website Link : https://www.thequantumprint.com/
Comments (0)